Sliding DU Bushing Factory Manufacturing Process and Quality Control
2026-11-01
Ever wonder what separates a sliding DU bushing that lasts from one that fails prematurely? At XIAYI, manufacturing isn't just about shaping metal—it's a precise choreography of sintering, sizing, and surface finishing, where every micron matters. Step inside our factory and you'll see how we control porosity, wall thickness, and friction coefficients long before the first truck hits the road. This isn't just quality control; it's a quiet obsession with the bushing's smallest details. Because when a DU bushing stops squeaking, the whole machine breathes easier.
From Powder Blend to Backing Strip
Every batch starts as a loose, carefully proportioned mixture of metal powders, binders, and lubricants. The blend isn't just dumped into a hopper—it's rolled and pressed through a series of calibrated steps that gradually transform the fluffy, inconsistent powder into a dense, uniform strip. Operators watch the feed rate and roll gap closely, because even a small shift in particle size or moisture can change how the material compacts. The goal at this stage isn't perfection, but predictability: a strip that holds together well enough to survive the next pass without cracking or delaminating.
Once the initial compaction happens, the strip passes through a sintering furnace where the binder burns off and the metal particles begin to fuse at their contact points. This isn't a full melt—the temperature stays below the main metal's melting point, so the strip remains porous but gains enough structural integrity to be handled. The backing strip emerges from the furnace with a slightly rough, matte surface and a dull metallic ring when tapped. Any irregularities here, such as uneven density or micro-cracks, will only amplify later during rolling or stamping, so the line speed and furnace profile are tuned by feel as much as by instrument readings.
After cooling, the strip is ready for secondary rolling to achieve the final thickness and surface finish. This step squeezes out much of the remaining porosity and aligns the metal grain structure, giving the backing strip its characteristic strength and flexibility. The edges are trimmed and the strip is coiled under controlled tension. The result is a continuous ribbon that looks almost nothing like the original powder blend—it's shiny, uniform, and quietly resilient. But trace the process backward, and every property of that finished strip traces back to how the powder was first blended, compacted, and sintered.
Sintering Steps That Shape the Porous Bronze
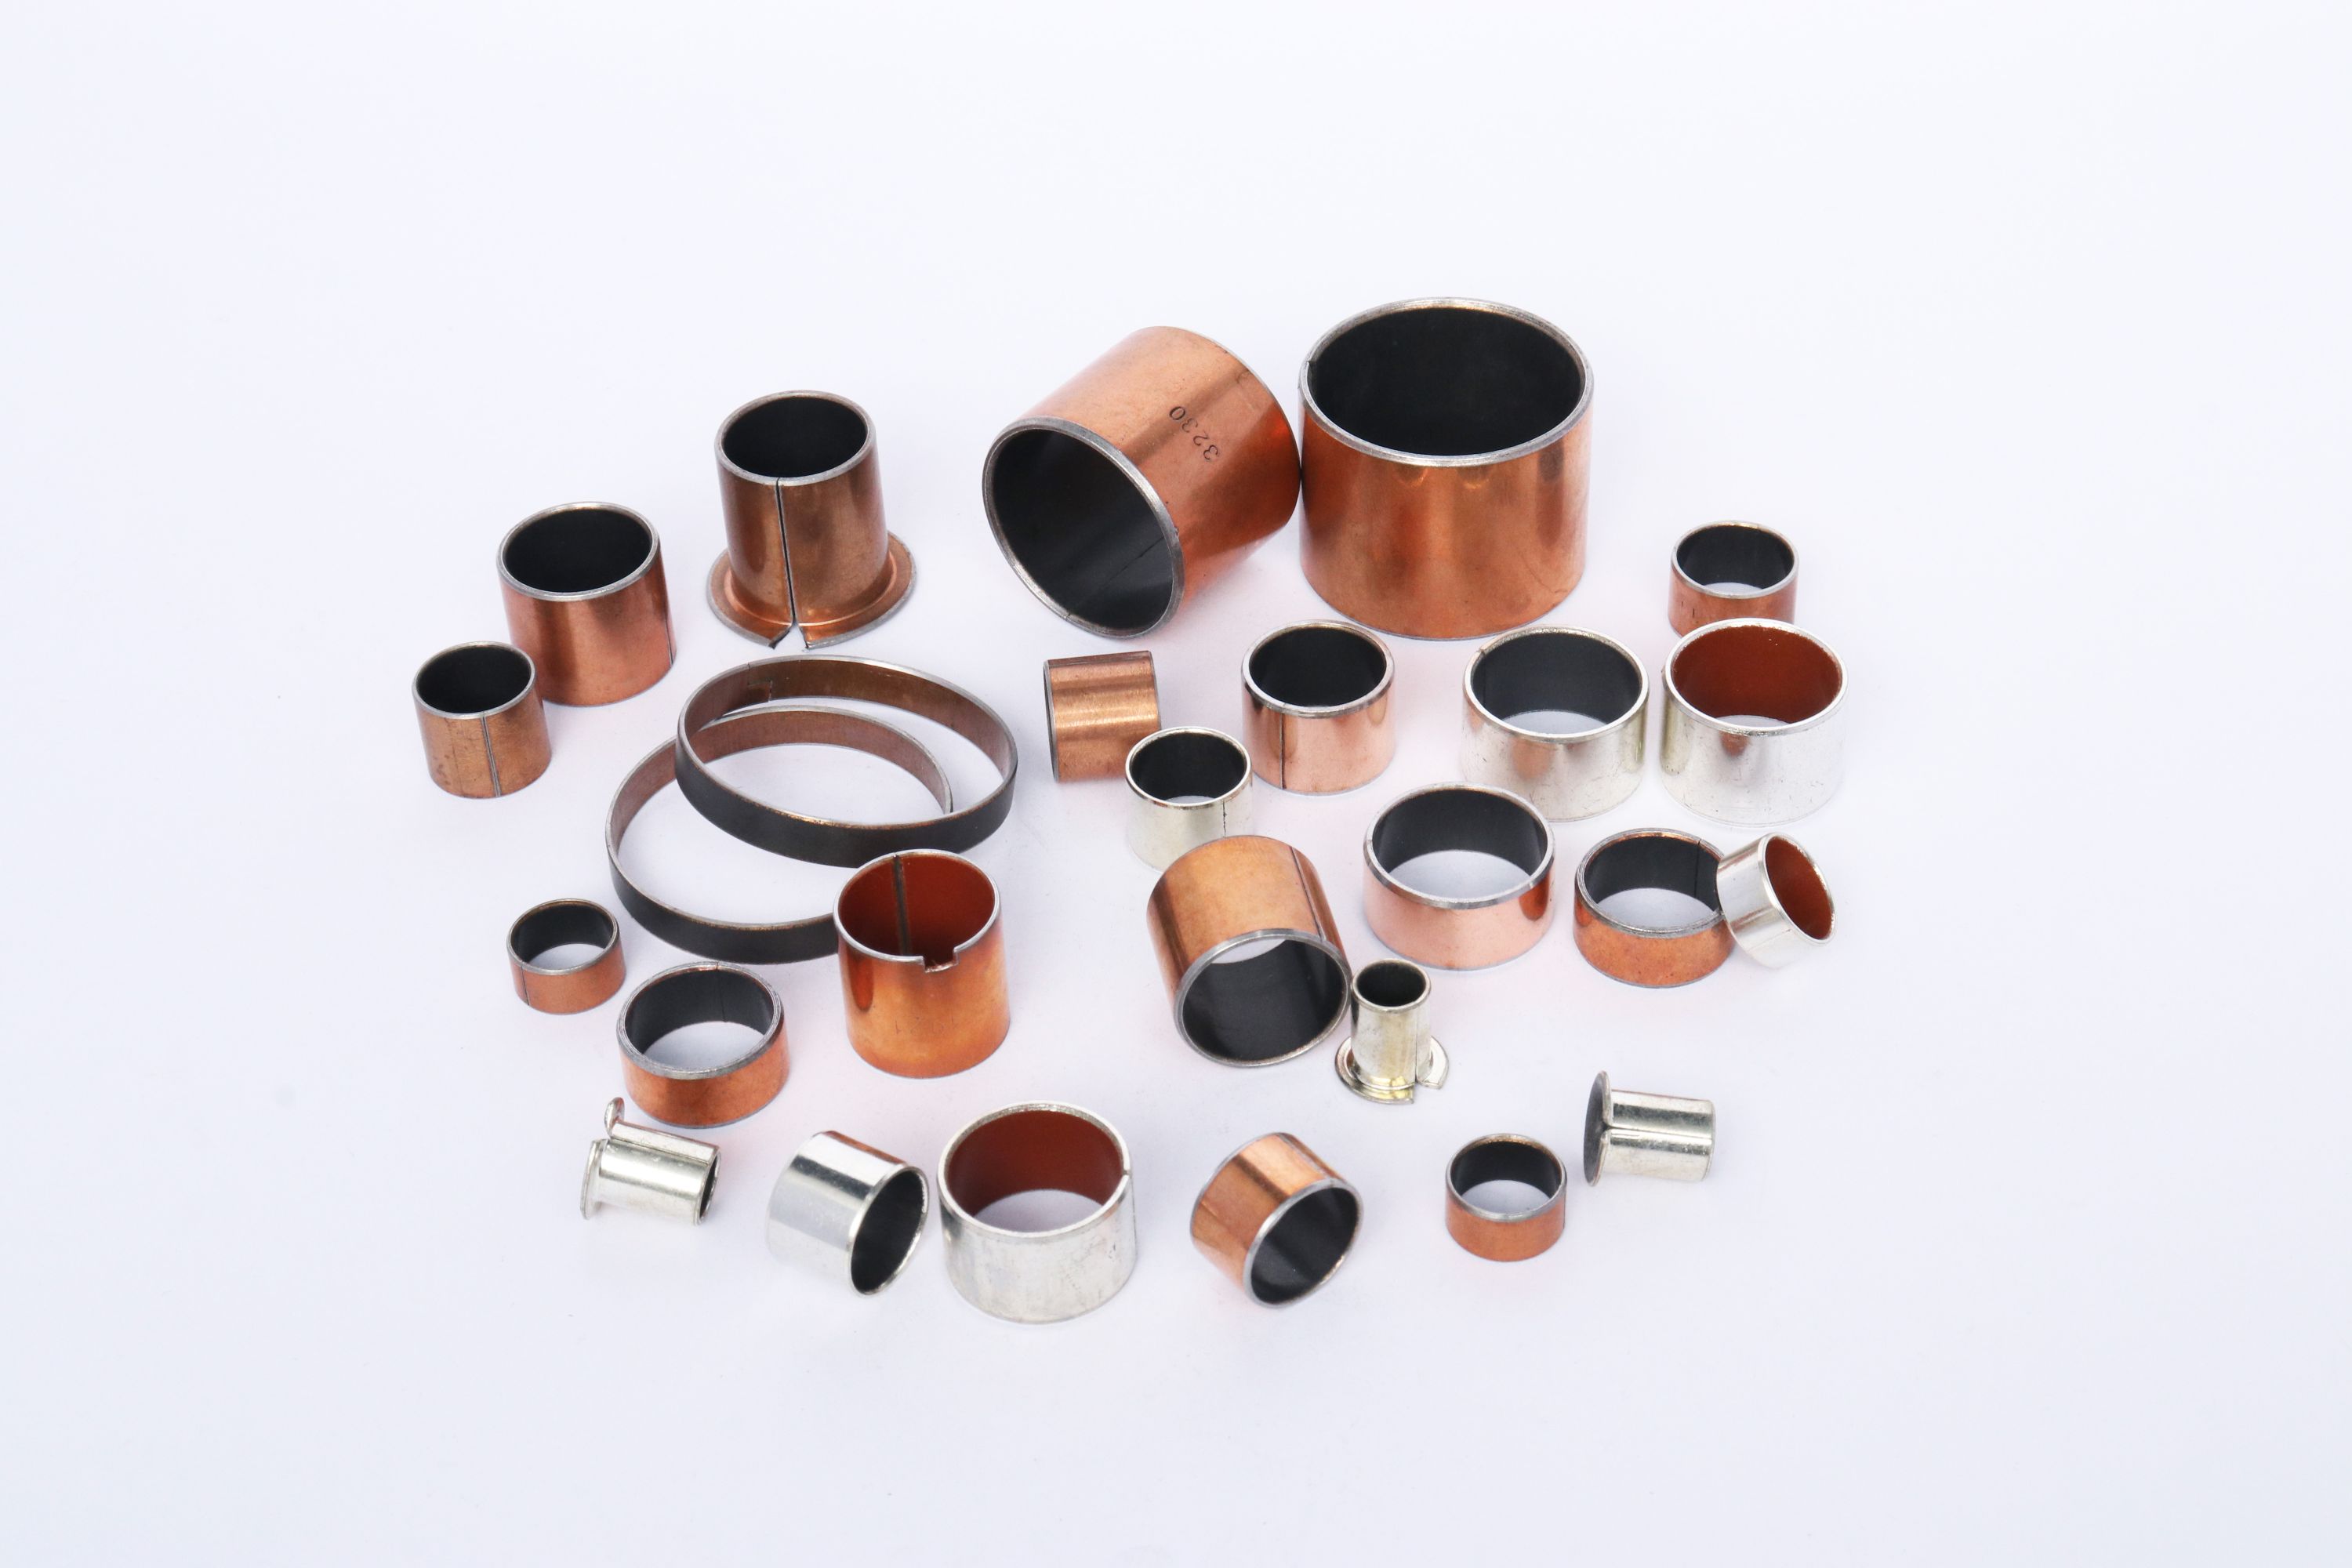
The transition from loose metal powder to a rigid porous structure begins with careful packing. Bronze particles are poured into a mold and lightly vibrated, encouraging them to settle without fully collapsing the spaces between grains. This initial arrangement determines the eventual pore size and distribution, so operators often adjust particle size blends to strike a balance between strength and permeability.
Once packed, the mold enters a controlled-atmosphere furnace where temperature climbs just below the melting point of the alloy. At this stage, atomic diffusion causes particles to bond at their contact points— a process known as necking. The trick is to hold the heat long enough to fuse the powder into a coherent skeleton, yet not so long that surface tension drives the pores to close. Even a few minutes of over-sintering can transform an open, breathable network into a dense solid.
Cooling then locks in the geometry. Rapid quenching introduces thermal stresses that may crack thin pore walls, so a gradual ramp-down is preferred. Some manufacturers introduce a brief secondary sintering pass at a slightly lower temperature to refine interconnections without further densification. The result is a porous bronze component whose final porosity, typically between 20 and 40 percent, reflects a delicate choreography of time, temperature, and particle architecture.
Drawing PTFE into the Pore Network
Getting PTFE to occupy the pores of a substrate without simply coating the surface calls for a combination of mechanical force and thermal softening. A common route is to lay a thin PTFE film over the porous body, then apply pressure while the assembly is held just above the resin's gel temperature. At that point, the polymer can flow enough to enter narrow channels, yet retains enough melt strength to avoid collapsing into void-free blobs. Repeated passes with a heated roller or a controlled vacuum on the opposite side help pull the material deeper, gradually replacing trapped air with a continuous PTFE phase.
The pore geometry dictates how far the PTFE travels before it locks in place. High-aspect-ratio capillaries with rough walls tend to grip the flowing polymer, slowing its advance but improving adhesion. In contrast, smooth, rounded voids allow easier penetration but may leave pockets where the PTFE retracts upon cooling. Adjusting the draw speed and the temperature gradient across the substrate lets you balance penetration depth against film thickness at the surface. Too aggressive a pull can tear the PTFE or create microfibrils that bridge pores instead of filling them, which is sometimes desirable in filtration media but problematic for dense sealing layers.
Once the PTFE is drawn into the pore network, the composite is cooled under pressure to freeze the structure before polymer relaxation sets in. Post-processing such as a brief sintering step can fuse the infiltrated strands with any remaining surface film, eliminating weak interfaces. The final distribution of PTFE within the network—whether it lines the pores as a thin sheath or nearly fills them—is controlled by the initial film thickness, the applied stress, and the number of draw cycles. This method is used to produce breathable membranes, hydrophobic filter elements, and low-friction bearing surfaces where the PTFE must survive repeated mechanical or thermal cycling without delaminating.
Sizing and Coining for a Tight Sliding Fit
Achieving a tight sliding fit means controlling the clearance between two mating parts so precisely that one can move over the other without noticeable play, yet still requires a deliberate push. The margin for error is often only a few microns, which makes standard machining alone unreliable for final dimensions. That's why post-processing steps like sizing and coining come into play, each addressing different sources of geometric variation.
Sizing typically refers to the careful removal or displacement of a small amount of material to bring a bore or shaft within the narrow tolerance band needed for the fit. Unlike rough machining, sizing often uses abrasive processes such as honing or lapping, which can remove as little as a fraction of a micron per pass. The operator measures the actual clearance at several points and adjusts the tool pressure or dwell time accordingly, working from the high side of the tolerance down rather than trying to hit the target in one shot.
Coining, on the other hand, is a cold forming operation that locally compresses the surface layer of a component to alter its dimensions or improve its surface integrity. In the context of a sliding fit, coining might be used to slightly expand a shaft diameter or to smooth out high spots left by previous machining. Because it relies on plastic deformation rather than cutting, coining can produce a very uniform surface with minimal material loss, and it often leaves behind residual compressive stresses that improve wear resistance. Used together, sizing and coining let a machinist dial in a tight sliding fit that feels smooth and consistent, without resorting to trial-and-error assembly.
In-Process Bond Checks Beyond the Visual
Visual inspection has long been the first line of defense against bond defects, but it misses what the eye cannot resolve. Subsurface cracks, void formation, and interfacial contamination often remain invisible under even high-magnification optics. Acoustic microimaging and X-ray tomography now penetrate beneath the bond line, revealing density shifts and delamination that would otherwise escape until field failure.
Bringing these methods into the process line changes the feedback loop from post-mortem to real time. Ultrasonic transducers mounted near the bonding head catch energy anomalies during formation, while thermal cameras track local heat dissipation as a proxy for contact area. Such signals feed directly into adaptive control algorithms that adjust force, power, and dwell time on the fly, reducing reliance on batch sampling.
The real shift is less about any single sensor and more about pattern recognition across multiple streams. When acoustic signatures, temperature profiles, and machine parameters are correlated, subtle drift becomes visible long before it produces a reject. Operators stop chasing scrap and start managing process capability, with fewer surprises at final test.
Simulating Real Loads Before Release
Shipping a feature without first mimicking the traffic it will face is like rehearsing a play in an empty theater. Real users arrive in bursts, linger on pages, abandon carts, and hammer the same endpoint at 2 a.m. because a notification just went out. A load test that only ramps up a flat number of requests per second misses these rhythms. Instead, capture production-like session flows—logins followed by searches, filter changes, pagination, and occasional timeouts—and replay them with realistic think times and arrival distributions. That’s where hidden bottlenecks tend to surface, not in a smooth synthetic curve.
Another piece that often gets skipped is variance across geography and device. A user on a throttled mobile connection in a rural area will hold connections longer and retry more aggressively than a desktop user on fiber. Simulating this means mixing latency profiles, packet loss, and slow DNS into the same scenario, not just increasing total throughput. It also helps to deliberately inject noise: random bursts of writes, oversized payloads from older app versions, and background sync jobs that fire during peak checkout. Systems that survive a homogeneous load can fall over when these edge patterns collide.
Finally, treat the pre-release simulation as a rehearsal for the on-call team, not just a pass/fail gate. Run the test during working hours, watch dashboards together, and document the first sign of saturation for each service. The goal is not to prove the system can handle N users; it’s to find the exact point where latency starts to climb and know which knob to turn before that point arrives in production.
FAQ
The starting point is a low-carbon steel strip for the backing, followed by a layer of atomized bronze powder. The bronze is sintered onto the steel to create a porous matrix, and then a PTFE-based compound mixed with lead or other fillers is rolled into those pores. No bulk PTFE tube or separate plastic liner is used.
Sintering fuses the bronze particles to the steel backing and to each other, but leaves controlled voids. Those voids act as reservoirs for the PTFE compound. If the furnace temperature or belt speed drifts, the pore size changes, which alters how much PTFE gets embedded and how well it stays put under load.
Rolling forces the PTFE paste into the sintered bronze pores under high pressure, filling the open structure without closing it off completely. Injection molding would create a solid plastic layer that cannot replenish the sliding surface as it wears. The rolling step also calipers the strip to a consistent thickness before forming.
After coining and sizing, operators measure inner diameter, outer diameter, and flange thickness at multiple points around the circumference. They also check the seam gap and the chamfer profile. Most factories use air gauges or digital bore micrometers rather than single-point calipers for production lots.
A representative sample is sectioned, mounted in resin, and examined under a microscope. The bond line should show no continuous oxide film or large voids. Some lines also run a peel test or a bend test where the strip is bent around a mandrel and inspected for separation.
A common test runs the bushing on a hardened steel shaft under a set load and speed, recording friction coefficient and wear depth over a fixed number of cycles. For example, a batch might need to stay below 0.15 coefficient of friction and show no scoring on the shaft after 50,000 cycles. Temperature rise is also logged.
The strip is rolled to a tight thickness tolerance before sintering. After forming, the bushing is sized in a precision die that sets the final OD and ID simultaneously. Wall thickness variation is then verified with an ultrasonic gauge on every nth part, with SPC charts tracking the range over the shift.
They are not reworked, because the bronze pore structure and PTFE layer cannot be restored once the part is formed. Failed parts are segregated, marked, and scrapped. The process engineers review the failure mode—whether it is a dimensional drift or a bond issue—and adjust the upstream parameters before the next batch.
Conclusion
At the heart of a sliding DU bushing factory lies a choreography of powder metallurgy and polymer infusion that turns raw copper, tin, and steel into a low-friction bearing surface. It starts with blending metal powders and spreading them onto a steel backing strip, then passing the layered material through a sintering furnace where controlled heat fuses the particles into a porous bronze matrix without collapsing the voids. The real magic happens next: a paste of PTFE and fillers is drawn under pressure into that open pore network, embedding a solid lubricant throughout the wear layer rather than merely coating it. After this impregnation, the strip goes through sizing rolls and coining dies that set the final wall thickness, inner diameter, and surface profile, producing a tight sliding fit that eliminates the need for a separate running-in period.
Quality control in this process refuses to rely on visual inspection alone. Bond integrity between the bronze layer and steel backing is checked with ultrasonic or peel tests, while porosity and PTFE fill depth are measured destructively on sample rings from each production lot. Before any batch ships, finished bushings are mounted in dedicated test rigs that replicate real-world load patterns, oscillating motions, and temperature cycles. Only parts that maintain a stable coefficient of friction and show negligible wear under simulated service conditions earn release. This combination of in-process bond verification and end-of-line performance simulation ensures that every sliding DU bushing leaving the factory behaves predictably in applications ranging from automotive suspensions to industrial actuators.
Contact Us
Contact Person: Leela
Email: [email protected]
Tel/WhatsApp: 8613586885132
Website: https://www.xiayishockparts.com